Hot Feed Rubber Extruder Manufacturer India — MI-HF-EXT Series
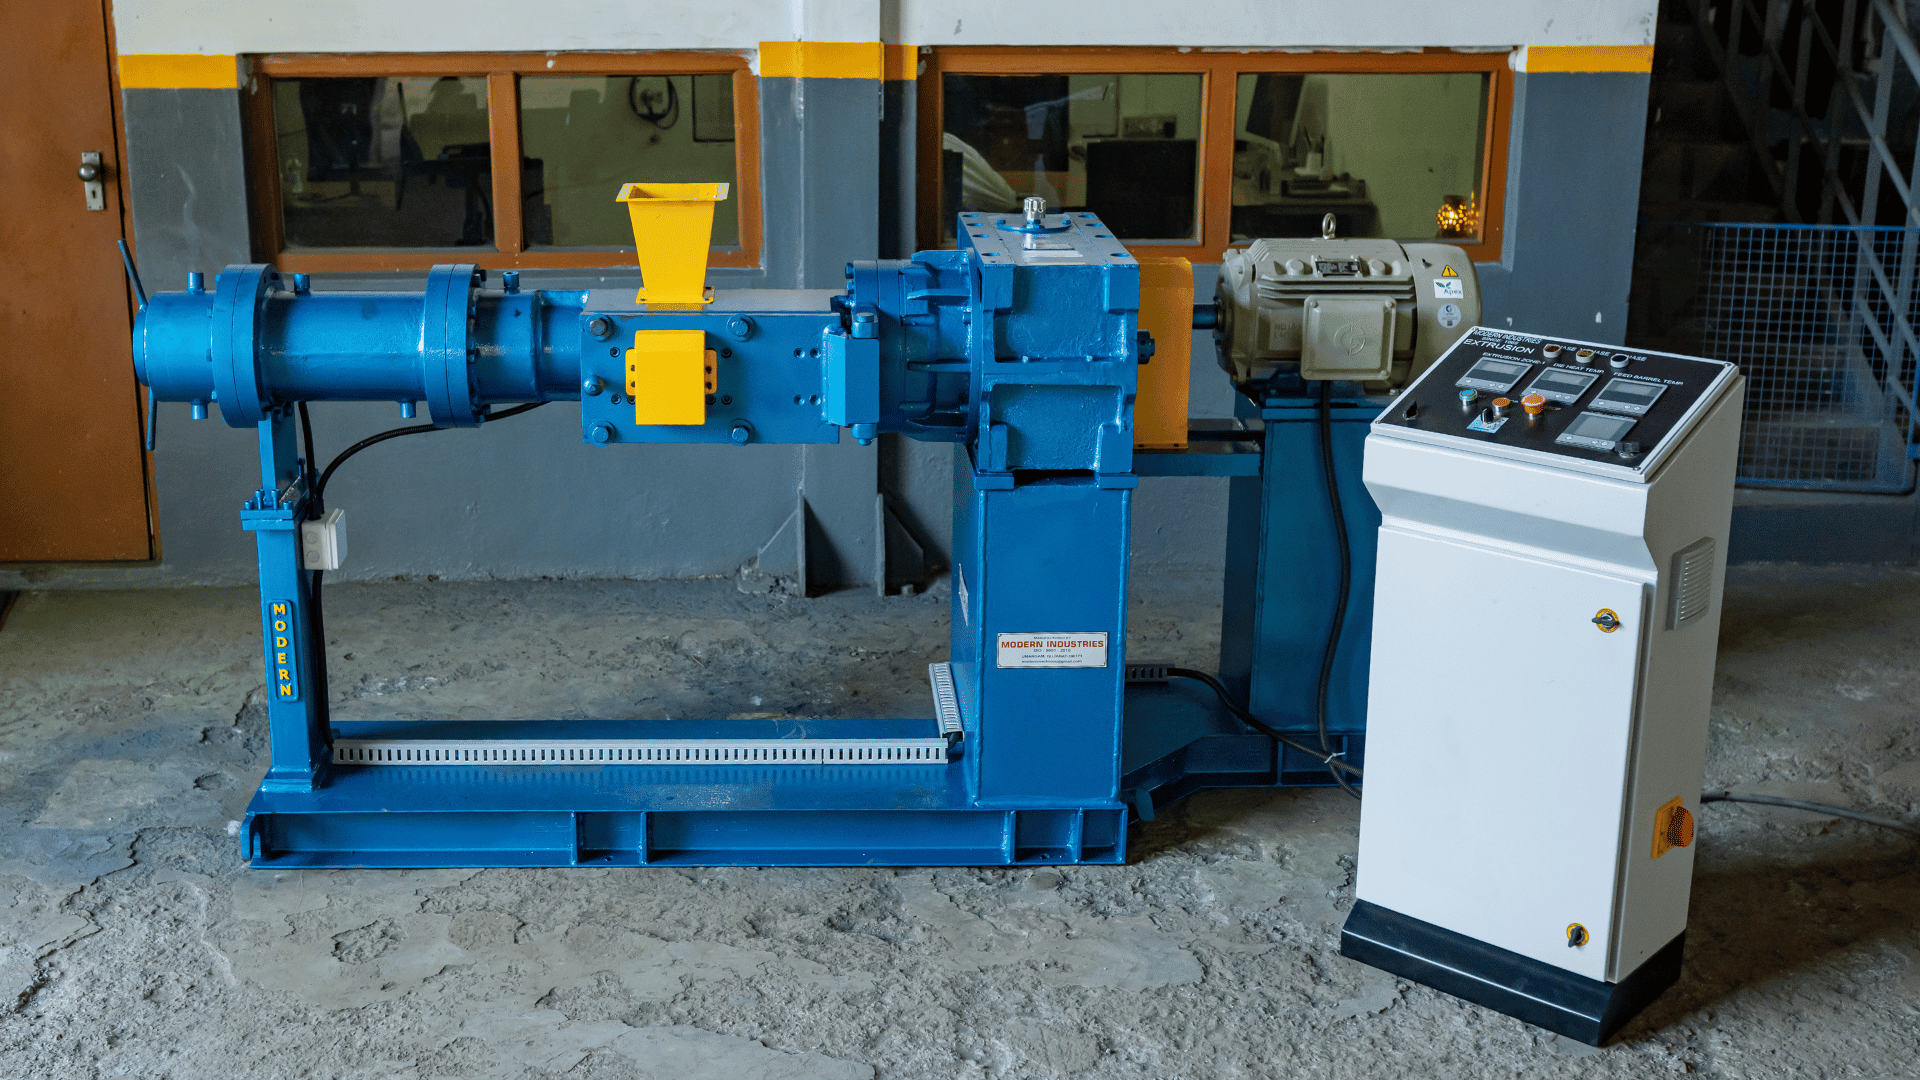
odern Industries Hot Feed Rubber Extruder — 7 models from 45mm to 200mm screw diameter. L/D ratio 6:1 on all models. Output 30–750 kg/hr. Built for high-output continuous extrusion of pre-heated rubber compound — tyre tread, rubber hose, profiles, tubes, and conveyor belt components.
What is a Hot Feed Rubber Extruder?
A hot feed rubber extruder processes compound that has been pre-warmed on a two-roll mixing mill before being fed into the hopper. Because the compound arrives already plasticised, the screw performs primarily conveying and shaping — not plasticising. This allows a short L/D ratio of 6:1 and high throughput for large cross-section profiles.
Hot feed extruders are the preferred choice where consistent high output matters more than extreme dimensional precision — tyre tread, large-bore hose, sponge profiles, rubber strips, and conveyor belt cover compound are all typical hot feed applications.
✓ MI-HF-EXT Series — Key Technical Highlights
L/D Ratio: 6:1 on all 7 models. Screw: EN-41B / 42CrMo4 nitrided alloy steel — single flight, low compression ratio.
Barrel: Nitrided alloy steel with hardened liner — extended wear life.
Head: Alloy steel, chrome-plated flow channels — smooth compound flow, easy die changes.
Drive: AC motor + helical gearbox + VFD — variable speed output control.
Cooling: Water circulation on barrel and die head — temperature stability.
MI-HF-EXT Series — Full Specification Table
All specifications verified from Modern Industries engineering data. Screw speed and TCU are not applicable on hot feed models.
| Model | Screw Dia (mm) | L/D Ratio | Motor (HP) | Output (kg/hr) | Cooling (lpm) | Weight (kg) |
|---|---|---|---|---|---|---|
| MI-HF-EXT-45 | 45 | 6:1 | 5 | 30-40 | 5 | 600 |
| MI-HF-EXT-55 | 55 | 6:1 | 7.5 | 40-45 | 10 | 750 |
| MI-HF-EXT-75 | 75 | 6:1 | 20 | 65-70 | 20 | 1,200 |
| MI-HF-EXT-100 | 100 | 6:1 | 30 | 125-150 | 40 | 1,800 |
| MI-HF-EXT-115 | 115 | 6:1 | 40 | 150-175 | 50 | 2,000 |
| MI-HF-EXT-150 | 150 | 6:1 | 100 | 300-400 | 75 | 4,000 |
| MI-HF-EXT-200 | 200 | 6:1 | 200 | 500-750 | 150 | 8,500 |
Construction & Materials
| Component | Specification |
|---|---|
| Screw | EN-41B / 42CrMo4 alloy steel, gas nitrided — single flight, low compression ratio |
| Barrel (Sleeve) | Nitrided alloy steel with hardened liner — wear-resistant inner surface |
| Head | Alloy steel with chrome-plated flow channels — smooth compound flow, reduced sticking |
| Drive | AC motor + helical gearbox + VFD — variable speed, overload protection |
| Heating | Electrical band heaters / cast aluminium heaters — zone-controlled temperature |
| Cooling | Water circulation system — barrel and die head temperature management |
| Frame | Heavy-duty fabricated steel base — grouted and bolted foundation mounting |
Temperature Zones — MI-HF-EXT Series
Hot feed extruders operate with 2–4 temperature zones depending on model size. All zones use electrical band heaters with water-circuit cooling. TCU (Temperature Controlling Unit) is NOT used on hot feed models — this is exclusive to the Cold Feed series.
| Zone | Location | Function |
|---|---|---|
| Zone 1 | Feeding Zone | Controls compound intake — maintains plasticity of pre-heated feed |
| Zone 2 | Extrusion Zone | Primary conveying and shaping zone |
| Zone 3+ | Additional Extrusion Zones | Present on larger models (75mm+) for extended processing |
| Zone 4 | Die Head | Die entry temperature — critical for profile dimensional consistency |
| Zone 5 | Screw | Internal screw temperature — prevents compound adhesion to screw surface |
Applications
Tyre Tread & Sidewall Extrusion
Hot feed extruders are standard for tyre tread extrusion — large-section NR/SBR profiles requiring consistent cross-section at high linear output. The MI-HF-EXT-150 and MI-HF-EXT-200 are used for full-width tyre tread extrusion lines.
Rubber Hose & Tube
General-purpose rubber hose — garden hose, low-pressure hydraulic hose, radiator hose, and air hose. Medium bore hose (ID 12mm to 75mm) is typically produced on MI-HF-EXT-75 to MI-HF-EXT-115 models.
Rubber Profiles & Strips
Solid and sponge rubber profiles for door seals, edge strips, gasket stock, and architectural sealing. The ability to run complex cross-section dies at high output makes hot feed standard for profile extrusion in building and industrial rubber goods.
Conveyor Belt Cover Compound
Top cover and bottom cover compound for conveyor belts is extruded on large hot feed machines. The MI-HF-EXT-150 and MI-HF-EXT-200 serve wide belt cover compound at 300–750 kg/hr.
Sponge & Cellular Rubber
Expanded rubber profiles for gaskets, seals, and cushioning products. Pre-heated compound allows blowing agents to activate consistently at the die exit.
Compatible Rubber Types
| Rubber Type | Grade Notes |
|---|---|
| Natural Rubber (NR) | All standard grades — RSS, SMR, Technically Specified Rubber |
| Styrene Butadiene (SBR) | SBR 1502, SBR 1712 — standard and oil-extended |
| Nitrile Rubber (NBR) | Low to medium ACN content — high ACN grades prefer cold feed |
| EPDM | All grades including high-filler EPDM for sponge applications |
| Butyl (IIR) | Standard and halogenated butyl — inner tube and bladder compound |
| Neoprene (CR) | Standard grades — flame-resistant profiles and hose |
| ECO / CSM | Specialty compounds — chemical resistant profiles and tubing |
Frequently Asked Questions
What is the difference between a hot feed and cold feed rubber extruder?
A hot feed extruder receives pre-warmed compound (40–70°C) from a mixing mill and uses a short screw (L/D 6:1) to convey and shape it. A cold feed extruder processes room-temperature compound — the longer screw (L/D 10:1–16:1) plasticises and shapes in one pass, with TCU temperature control per zone. Hot feed delivers higher throughput for large-section profiles; cold feed is preferred for precision profiles and tight dimensional tolerances.
What is the price of a hot feed extruder in India?
Price depends on screw diameter, motor power, and die configuration — ranging from MI-HF-EXT-45 (45mm, 5 HP) to MI-HF-EXT-200 (200mm, 200 HP). Contact our sales team at +91 90004 00334 or sales@modernrubbermachinery.com for a quotation based on your specific requirement.
Which MI-HF-EXT model is best for tyre tread extrusion?
Tyre tread extrusion typically requires MI-HF-EXT-150 (100 HP, 300–400 kg/hr) or MI-HF-EXT-200 (200 HP, 500–750 kg/hr) for full-width tread profiles. For narrow tread strips and sidewall profiles, MI-HF-EXT-100 or MI-HF-EXT-115 may be sufficient. Contact us with your tread profile width, thickness, and output requirement for a specific recommendation.
Can a hot feed extruder process EPDM compound?
Yes. EPDM — including high-filler sponge EPDM — is a standard compound for hot feed extruders. EPDM sponge profiles for door seals and weatherstripping are a primary hot feed application. Ensure compound is properly warmed on the mixing mill before feeding for consistent output and surface quality.
What is a strainer extruder?
A strainer extruder is a variant of the hot feed extruder fitted with a breaker plate and strainer screen between the screw and die head. The screen filters foreign particles and undispersed ingredients from the compound before die entry — essential for technical rubber goods and applications requiring clean, contamination-free compound. Modern Industries can advise on strainer extruder configurations across the MI-HF-EXT range.